


| Newspaper Articles |

|
Newspaper Articles |
 |
 |
26th December 1942, Page: 148, Column: 1
Electricity In Mine Pumping
Extracts from paper on "The Application of Electricity in Mine Pumping" prepared for presentation to the Installations Session of the Institution of Electrical Engineers. Date of meeting 10th December.
By G. B. Alvey and N. Tetlow.
Although centrifugal pumps are adopted for the greater range of mine-drainage duties, there are some duties for which they are not always suitable or economical.
To apply a centrifugal pump successfully to mine-drainage work, it is first essential to have a knowledge of the hydrodynamic characteristics of the pump and of the pipework system through which it is required to discharge.
A centrifugal pump is designed for the specific duty for which it is required, and its maximum efficiency occurs at one rate of flow and one corresponding net generated head.
The speed for which a centrifugal pump may be designed is determined by many factors, the chief of which are :—
(a) The hydrodynamic characteristics required. The pump designer's measure of the type of pump is its specific speed, where
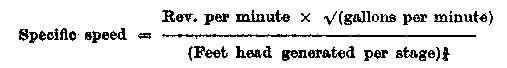
all these factors being measured at the point of maximum efficiency
(b) The suction performance, or "suction ability" of the pump. This is one of the most important factors influencing the running speed of a pump. The peripheral velocity of the vanes at the impeller eye must not, for instance, exceed the figure at which cavitation takes place.
Sinking and Unwatering Pumps.
During the operation of sinking a mine shaft it is, in general, necessary to provide pumping equipment capable of removing water from the shaft. A pumping unit of this type, known as a sinking pump, must be completely self-contained and must be capable of being moved down the shaft as sinking proceeds. A similar operation from the point of view of pumping is that of unwatering a mine which has been allowed to fill with drainage water.
Sinking and unwatering pumps may be either of the centrifugal or of the positive-displacement type, depending on the duty. The pump, with its driving motor, suction pipe line and valves, is generally built into a fabricated steel framework which is suspended in the vertical shaft and can be raised or lowered at will. Ability to deal with high-suction-lift conditions is an essential feature because drainage or unwatering can only proceed in steps which are limited by the suction ability of the pump.
There is a growing tendency to-day in British collieries to centralise mine-drainage pumping. Disused colliery workings are frequently used for this purpose and serve as central drainage points for several collieries. If the shaft is used only for pumping, the surface winding engine and gear may be removed, so avoiding heavy maintenance costs, routine inspections, etc. Still further savings can be effected by installing pumping sets of the fully automatic type requiring only occasional routine inspection. Automatic pumping sets of this type are usually float-operated from the level of the water in the sump.
If automatic pumping equipment is to be a success, certain important factors must be taken into consideration. Precautions must be taken to ensure that the pump remains fully primed, or is provided with equipment to prime it automatically when necessary. A ram pump is self-priming within reasonable limits of suction life. A centrifugal pump, on the other hand, must be provided with priming equipment.
For driving centrifugal pumps in mines, motors of small, medium and large capacity are required, usually direct-coupled to the pumps. The drives are easy, and only comparatively light starting torques are required. For ram pumps, small- or medium-capacity motors are usually required, and there is reasonable freedom in the selection of motor speed because the pumps are almost invariably driven through gears. Ram pumps often start under heavy load.
The driving of mine sinking pumps presents a case where the utmost simplicity of motor and control gear is especially desirable.
The operation of the motor is sometimes controlled from the surface of the mine, in which case three conductors only are required where direct-on-started squirrel-cage machines are installed, as against the six conductors which are necessary between motor and surface where wound-rotor or star-delta-started squirrel-cage machines are employed. If controlled from the sinking pump staging a wound-rotor motor or a fractional voltage-started squirrel-cage motor requires additional control gear and connections on the staging, whereas the direct-on-started machine requires only a triple-pole switch of the simplest type and readily affords the necessary mechanical protection. Another objection to the wound-rotor machine lies in the reduced reliability resulting from its insulated rotor winding and slip-rings, under the arduous conditions imposed by this service, including the probability of considerable vibration. A squirrel-cage motor is obviously much better able to contend with such severe conditions.
The type of motor and method of starting employed for pumping service in a mine may affect the characteristics of the whole of the switchgear installation, particularly if the pump motors are large compared with other motors in the mine. For example, the overload protective features of all switches in circuit with such motors must withstand the starting currents and afford at least short-circuit protection to the cables. For normal squirrel-cage motors, started on fractional voltage, the initial starting currents are usually relatively low, but at change-over from fractional to full voltage heavy transients occur. Heavy transients are also liable to occur when wound-rotor motors are switched in circuit.
With squirrel-cage motors designed for direct-on switching with low starting current, however, it is unusual to find high transient currents at switching-in. On the other hand the switch-gear must be designed to deal with a relatively high current maintained for a few seconds. It is obvious that this requirement may necessitate features in the main switchgear differing from those required for other starting methods.
Motors of medium and large sizes driving main drainage pumps in mines are usually of the ventilated type with drip-proof or splash-proof enclosure. Squirrel-cage induction-type motors are almost unaffected by any reasonable amount of dirt, and since these motors usually run for long spells, without extended idle periods, the windings are quite unaffected by ordinary humid atmospheres, provided they are suitably insulated and impregnated. Direct-current motors, which are much more susceptible to the effects of dirt and grit, may with advantage be provided with an air filtering system.
Main drainage pumps in collieries are often installed at or near the bottom of the downcast shaft, and the motors in such cases may therefore be of the ventilated type, but conditions sometimes require flameproof construction. Auxiliary drainage pumps, being frequently installed near to the coal face, more usually require motors of flameproof design. If a fully flameproof motor is required, total enclosure of the whole machine is of course essential, and the incidental advantages and disadvantages of this type of enclosure must be accepted.
When, as is usual in colliery practice, the main pumping plant is installed at or near to the bottom of the downcast shaft, it is an easy matter to provide an adequate supply of fresh air for the purpose of cooling the motors. In other mines, large motors are often installed in situations where the supply of fresh air is insufficient to carry away the heat generated in the motors. The pump chambers are often cut out of solid rock, therefore being of the smallest possible dimensions, and the walls themselves are unable to absorb sufficient heat to keep the circulating air cool.
For main or auxiliary drainage pumps a fully flameproof motor is sometimes necessary. Then total enclosure of the whole machine is, of course, essential and the incidental advantages and disadvantages of this type of enclosure must be accepted. Flameproof motors for use in mines in this country must be covered by a certificate of flameproofness issued by the Mines Department of the Board of Trade.
Where a ventilated motor is in almost continuous service, it is only necessary to protect the windings from falling water, even in very damp situations. If duplicate sets are installed, running during alternate periods, the windings will usually remain sufficiently dry, but in some situations it may be worth while to convey the warm air expelled from the running machine, or a portion of it, to the idle machine.
If a motor is on irregular or very intermittent duty, some means of maintaining the windings warm and dry should be adopted. In the case of d.c. motors, one method might be to pass current through the shunt field coils whenever the motor is stationary. For a.c. motors the ideal method is to switch low-voltage current through the stator windings, automatically, when the-motor stops. The supply may be taken from a suitable step-down transformer, and adequate heating current is usually insufficient to turn the motor when coupled to a pump. Alternatively, electric space heaters, also automatically controlled, may be installed and suitably disposed in the motor frame.
 |
 |
| Names mentioned in this article | |
 |
 |
| Name | Age | Occupation | Notes |
|---|---|---|---|
| Alvey, G. B. | |||
| Tetlow, N. |




 Contains public sector information licensed under the

